01
Laser cutting
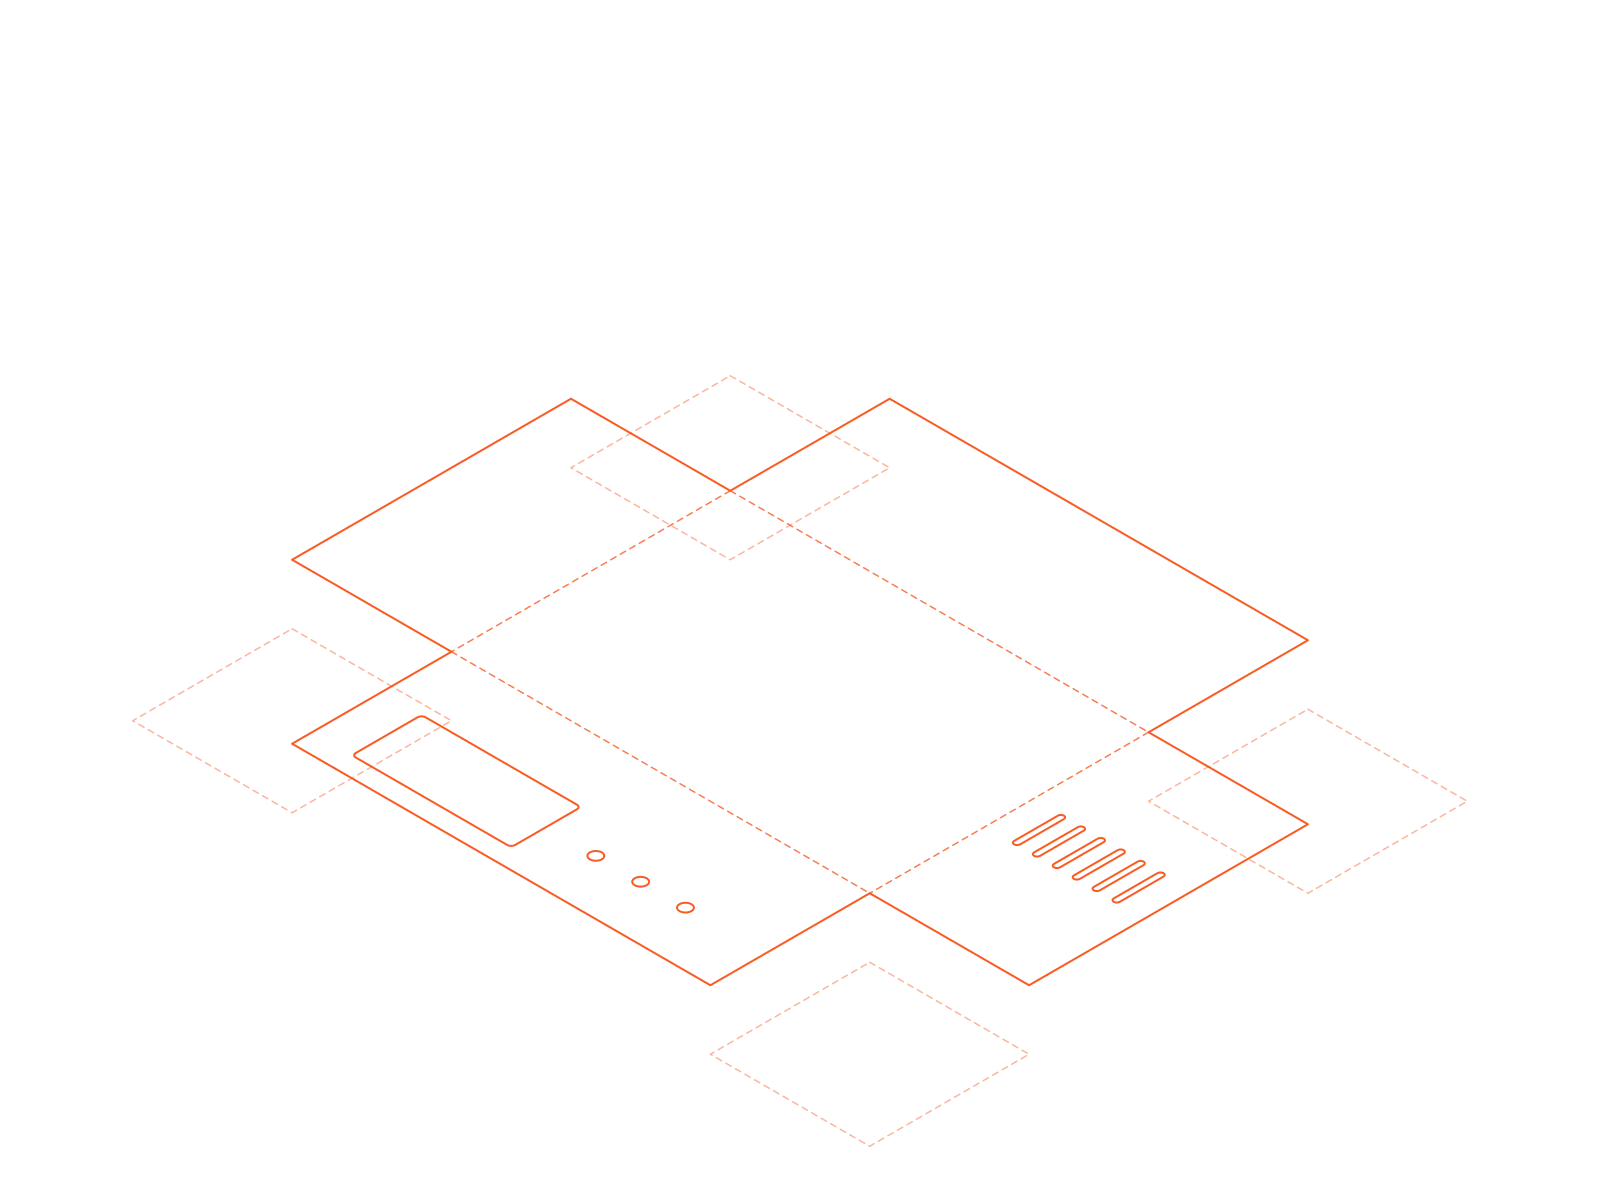
A 2 mm CRCA steel blank is cut on a 6 kW fiber laser — vents and display window included.
- Nitrogen-assist cut: clean, oxide-free edges
- Nested to cut the blank with under 6% scrap
- Every part laser-marked with a traceable ID
Ironvale · Contract manufacturing · Pune · Monterrey · Austin
Sheet metal, machining, finishing and box-build assembly for OEMs — engineered, built and inspected in our own facilities.
A manufacturing engineer replies within 1 business day.

Now watch us make it.
01
A 2 mm CRCA steel blank is cut on a 6 kW fiber laser — vents and display window included.
02
Four flanges are formed to 90° on a CNC press brake in a single setup.
03
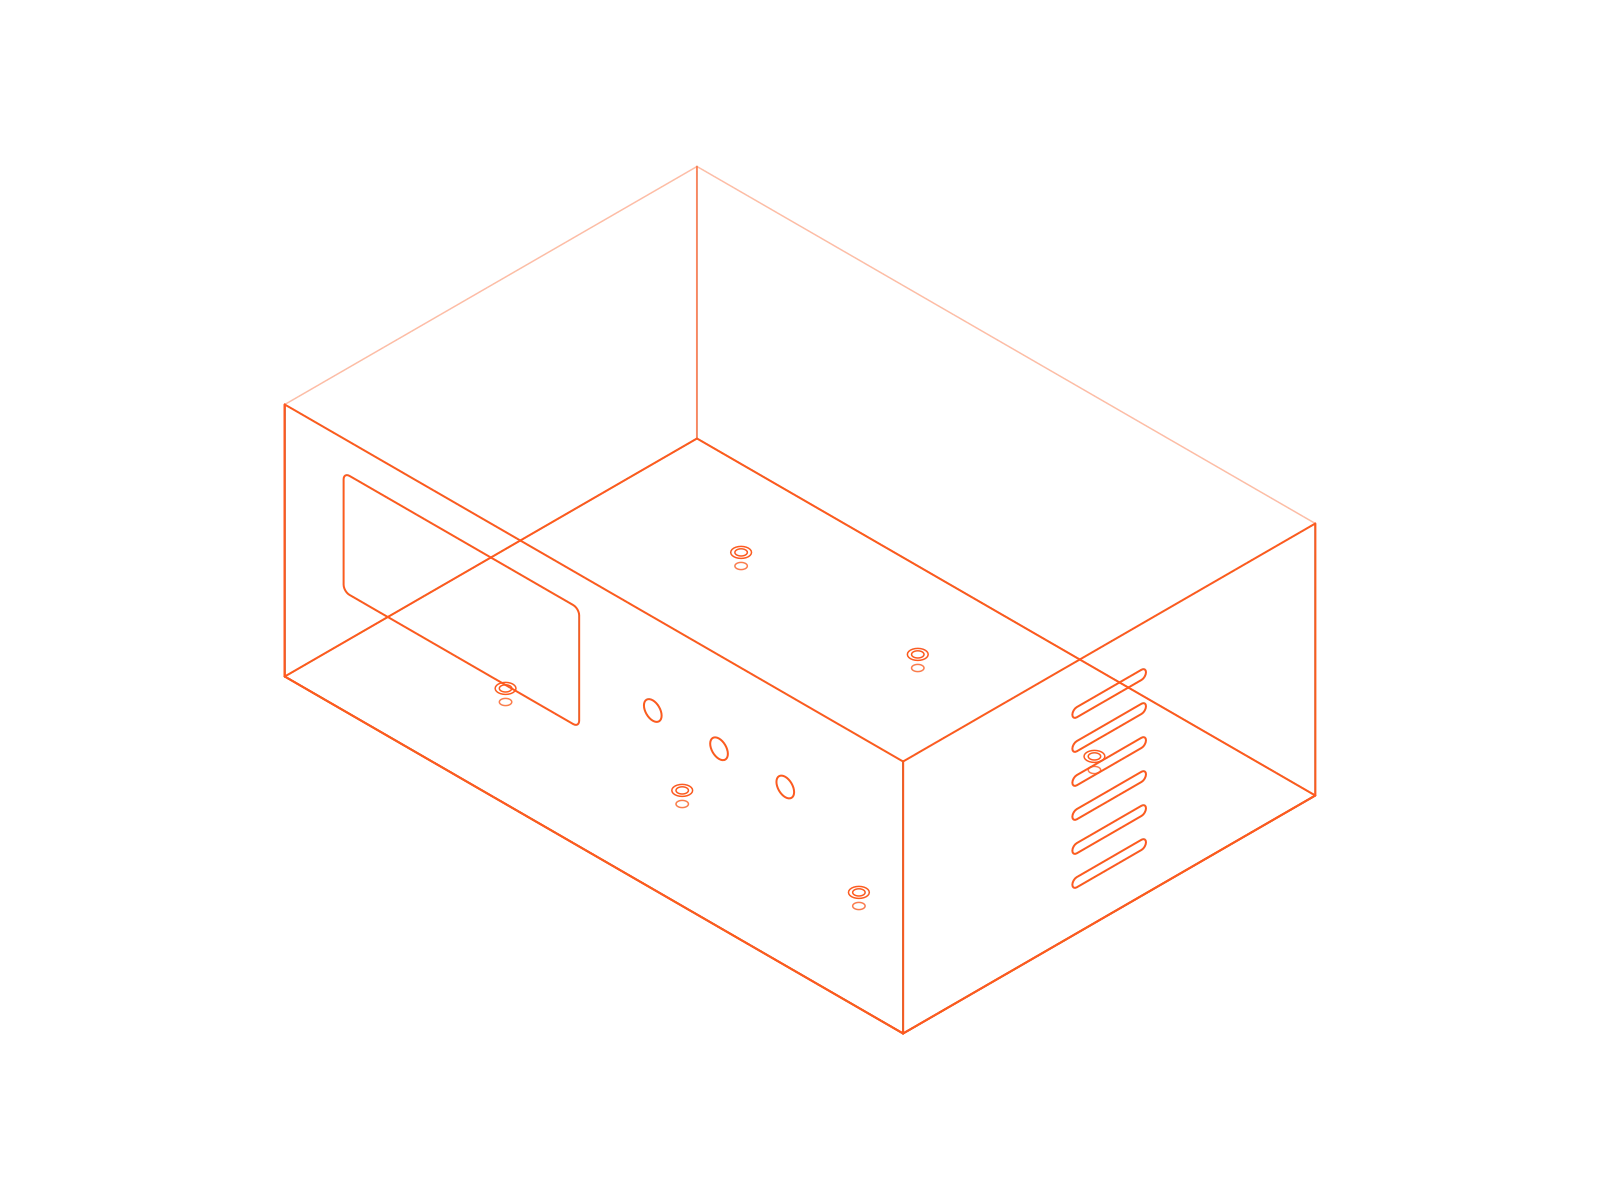
M4 PEM studs are pressed in; corners are TIG-welded and dressed.
04
Pre-treated and powder coated for a durable, even finish.
05
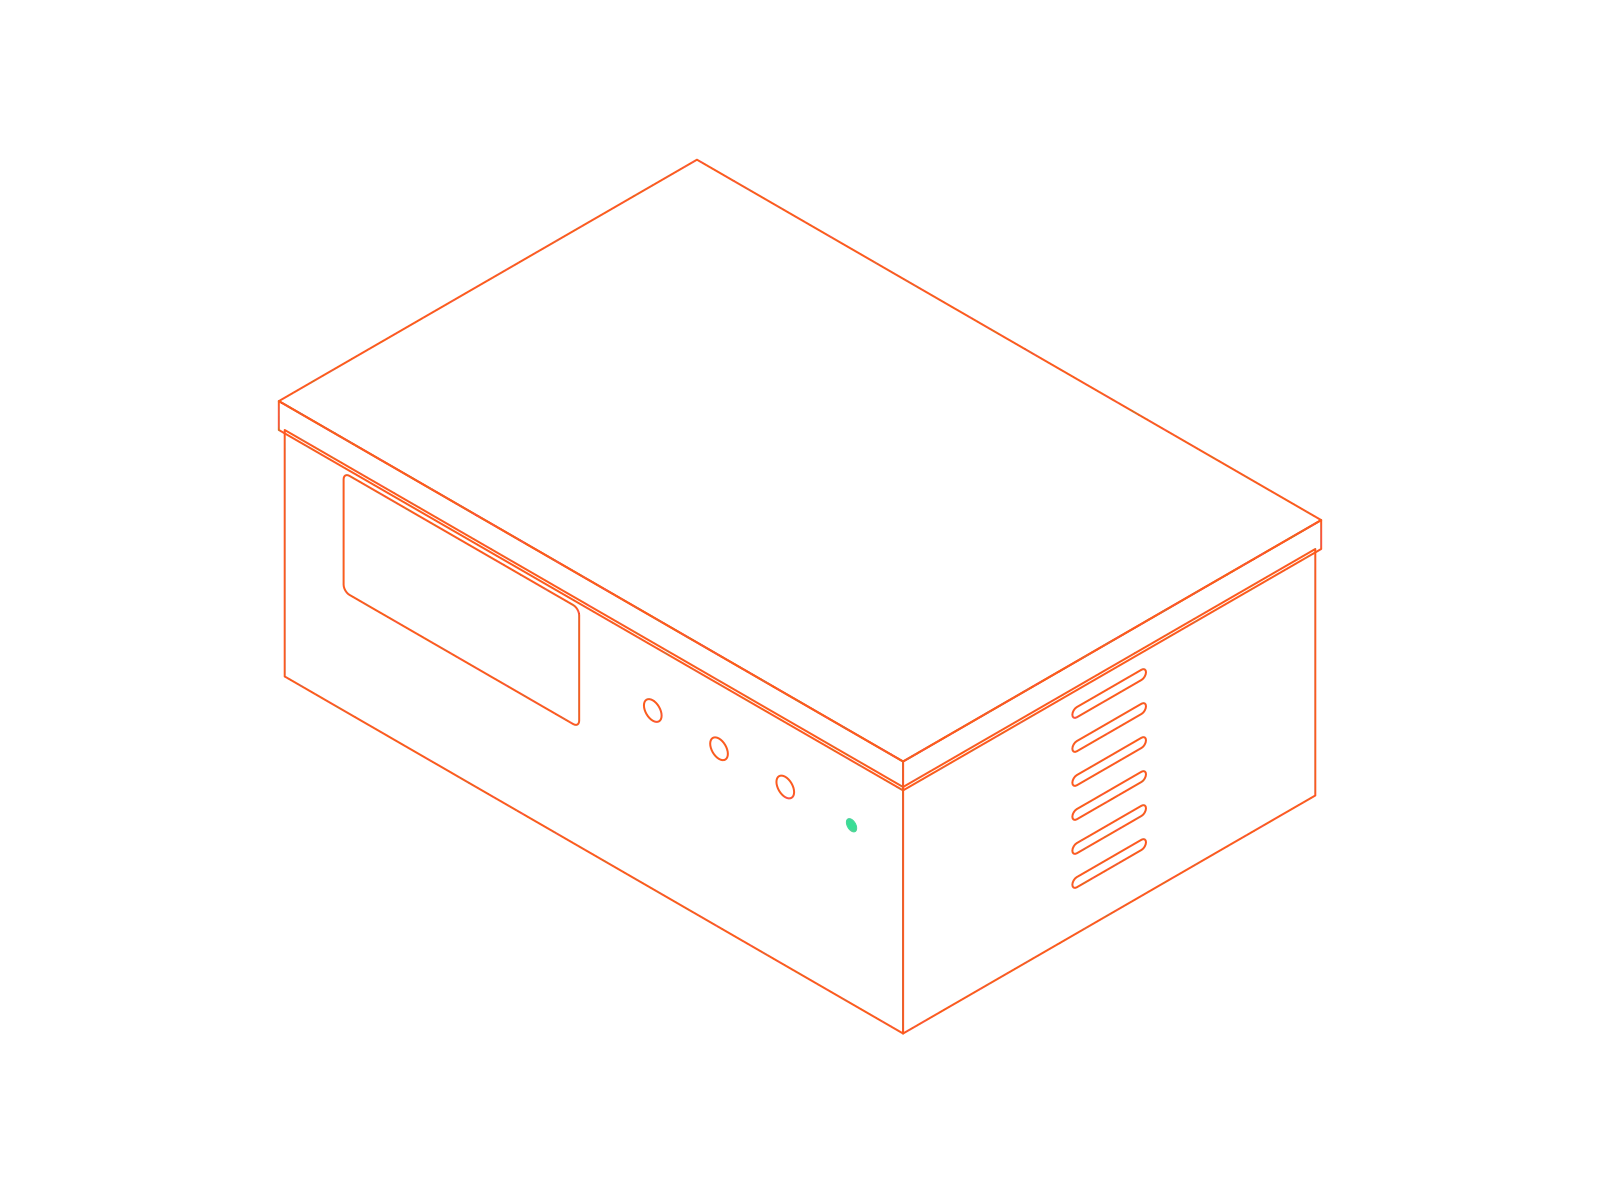
Lid, front panel and electronics are fitted, and every unit is tested before it ships.
QC PASSED
01
A 2 mm CRCA steel blank is cut on a 6 kW fiber laser — vents and display window included.
Fiber laser · ±0.05 mm
02
Four flanges are formed to 90° on a CNC press brake in a single setup.
Bend · 90.0° ±0.5°
03
M4 PEM studs are pressed in; corners are TIG-welded and dressed.
M4 PEM × 6 · TIG corners
04
Pre-treated and powder coated for a durable, even finish.
RAL 9002 · 80 µm
05
Lid, front panel and electronics are fitted, and every unit is tested before it ships.
100% functional test
Capabilities
Six processes, run on our own lines in three facilities. Each one is set from your drawing and checked before the next step starts.
Laser cutting, punching, press-brake forming and resistance welding for enclosures and chassis.
Milling and turning of brackets, heat sinks and precision mounts in aluminium, steel and stainless.
TIG and MIG welding, with PEM studs, nuts and standoffs pressed in during the sheet-metal run.
Pre-treatment, electrostatic powder coat and cure in-house, with anodising and passivation through qualified partners.
Harness, board and panel integration, torque-logged fastening, labelling and ESD-safe packing.
Prototypes from the same process route as production, moved to hard fixtures and tooling without a redesign.
Industries
The enclosures and frames we make every week, and the parts that go inside them.
Outdoor cabinets, rack frames and heat-sinking brackets for base stations and switches.
Charger housings, power-module chassis and cable-management brackets.
Stainless instrument housings, washdown-rated covers and tray frames.
Control cabinets, operator panels and DIN-rail mounting plates.
Switchgear panels, busbar supports and metering enclosures.
Chamber frames, service panels and cover assemblies for clean-room tools.
Materials & tolerances
Typical values for production sheet parts. Your drawing sets the tolerance; these are the defaults we quote against.
| Material | Thickness range | Typical tolerance | Common finishes |
|---|---|---|---|
| CRCA steel | 0.8–3.0 mm | ±0.10 mm laser · ±0.5° bend | Powder coat, zinc plate |
| Galvanised steel | 0.8–2.5 mm | ±0.15 mm laser · ±0.5° bend | Clear chromate, powder coat |
| Stainless 304 / 316 | 0.8–3.0 mm | ±0.10 mm laser · ±0.5° bend | Passivation, brushed #4 |
| Aluminium 5052 / 6061 | 1.0–6.0 mm | ±0.15 mm laser · ±0.5° bend | Clear or black anodise, powder coat |
| Copper C110 | 0.5–3.0 mm | ±0.10 mm laser · ±0.5° bend | Tin plate, bare |
Facilities
One quality system and one set of work instructions across all three sites, so a part qualified in one can be built in another.
Sheet-metal fabrication and press-brake forming for high-volume enclosures.
CNC machining, welding and box-build assembly, with a dedicated electronics cell.
Prototypes, first-article builds and new-product introduction before volume moves to Pune or Monterrey.
Quality
Four gates between incoming steel and the box on the pallet. Each gate keeps its own record, and the records ship with the lot.
Gate 01
Mill certificates are checked against every heat and coil before cutting starts.
Gate 02
Critical dimensions are sampled on the line and charted, and parts are held when a reading drifts toward a limit.
Gate 03
The first part off every new setup is measured in full on a coordinate measuring machine.
Gate 04
Every unit is powered and exercised on a test rig before it leaves the building.
Certifications · sample data
Quoting
Step 01
Upload a STEP, DXF, DWG or PDF with quantities and target finish. A rough sketch is enough to start.
Step 02
An engineer checks bend radii, hole spacing and tolerances, and flags anything that drives cost.
Step 03
You get a fixed-price quote, a lead time and the DFM notes. Nothing starts until you approve it.
Resources
Bend radii, hole-to-edge rules, relief cuts and flange lengths, with worked examples.
Request the PDF for the DFM guideTypical fit and form tolerances by process, from laser cut to CNC mill, on one page.
Request the PDF for the tolerance cheat-sheetCRCA, galvanised, stainless, aluminium and copper compared on strength, corrosion and cost.
Request the PDF for the material selection guideSample answers for this concept demo.
Prototype runs start at one unit. Production orders typically start at 50 units, and smaller batches are quoted case by case.
STEP and DXF are preferred for geometry, with a PDF drawing for tolerances and finishes. Native DWG and SolidWorks files are accepted on request.
Prototypes take 5 to 7 business days. Production orders take about 3 to 4 weeks after approval, depending on finish and quantity.
All three sites run under ISO 9001 and IATF 16949. These are sample certifications for this demo.
We ship by LTL freight or parcel and quote DAP (delivered at place) as standard. EXW and FCA are available if you use your own forwarder.
Yes. Prototypes come off the same laser and press-brake routes as production, so the first run tests the real process, not a hand-built stand-in.
Send a drawing or a rough idea. We'll come back with a DFM review and a quote.
Concept demo by UnitOne AI · company name and figures are sample data
(Demo: nothing was sent.)